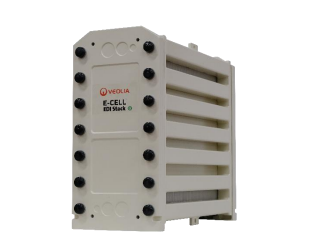
Veolia Electrodeionization EDI Stack Modules
E-Cell™ EDI MK-9 Stack for Power Generation, Solar Manufacturing & Green Hydrogen
High-Capacity Ultrapure Water Production with Continuous, Low-Chemical OperationThe E-Cell™ EDI MK-9 Stack delivers a reliable, continuous supply of ultrapure water for demanding industrial applications.Designed for power generation, solar panel manufacturing, green hydrogen production, and other h
High-Capacity Ultrapure Water Production with Continuous, Low-Chemical Operation
The E-Cell™ EDI MK-9 Stack delivers a reliable, continuous supply of ultrapure water for demanding industrial applications.
Designed for power generation, solar panel manufacturing, green hydrogen production, and other heavy industrial processes, the MK-9 uses electrical current to continuously regenerate the ion exchange resin inside the stack. This eliminates the need for routine acid or caustic regeneration while supporting stable water quality, high recovery, and efficient operation.
With a nominal flow rate of 8.0 m³/h (35.2 gpm) , the E-Cell™ EDI MK-9 provides a practical, high-capacity solution for facilities that need dependable demineralized or ultrapure water without the complexity of conventional chemical regeneration.
High-Purity Water for Critical Industrial Processes
Water quality directly affects equipment protection, process reliability, and operating performance. The E-Cell™ EDI MK-9 Stack is engineered to produce high-purity water for applications where consistency matters.
Product water performance
Resistivity of up to ≥16 MΩ·cm
Sodium concentration of ≤3 ppb
Silica levels as low as 5 ppb
Sodium removal of ≥99.9%
Silica removal of up to 99%
Recovery of up to 97%
Actual performance may vary depending on feed water quality, flow rate, temperature, system configuration, and site conditions. Performance projections and available guarantees can be verified using the Winflows® Design Simulator or through a Veolia representative.
Built for Demanding Industrial Applications
The E-Cell™ EDI MK-9 Stack delivers the consistent water quality required by high-performance industrial systems.
Power generation
Produce demineralized boiler feedwater for high-pressure boilers in power plants and heavy industrial facilities. High-purity feedwater helps protect steam-cycle equipment and support reliable plant operation.
Solar panel and microelectronics manufacturing
Provide ultrapure rinse water for solar panels, electronic components, and other sensitive manufacturing processes where ionic contamination can affect product quality.
Green hydrogen production
Supply ultrapure water for electrolyzer systems used in green hydrogen generation, helping support efficient and reliable hydrogen production.
Heavy industry
Integrate the MK-9 into industrial water treatment systems that require continuous, high-quality demineralized water with reduced chemical handling.
Continuous EDI Performance Without Routine Chemical Regeneration
The E-Cell™ EDI MK-9 uses electricity to continuously regenerate the ion exchange resin within the stack. This simplifies operation and reduces dependence on hazardous regeneration chemicals.
Key advantages
Continuous production of ultrapure water
No routine acid or caustic regeneration
No brine injection
No concentrate recirculation
High water recovery of up to 97%
Low energy consumption
Reduced operator intervention
Counter-current operation to help minimize cleaning requirements at higher feed water hardness levels
Compact design for integration into RO-EDI systems
Leak-free operation supported by a standard 3-year prorated warranty
By reducing chemical requirements and manual maintenance activities, the MK-9 helps simplify water treatment operations while maintaining the performance expected from a modern EDI system.
High Capacity in a Compact Stack Design
| Specification | E-Cell™ EDI MK-9 Stack |
|---|---|
| Nominal flow rate | 8.0 m³/h / 35.2 gpm |
| Flow rate range | 4.2-10.0 m³/h / 18.5-44.0 gpm |
| Recovery | Up to 97% |
| Maximum inlet pressure | 6.9 bar / 100 psi |
| Dimensions, W × H × D | 30 × 61 × 74 cm / 12 × 24 × 29 in |
| Shipping weight | 165 kg / 364 lb |
Pressure drop and electrical operating parameters should be confirmed for the specific system design and operating conditions using the Winflows Design Simulator.
Designed for RO Permeate Feedwater
The E-Cell™ EDI MK-9 Stack is designed to operate with reverse osmosis permeate or equivalent-quality feedwater. Proper pretreatment helps protect the ion exchange media from particulates, colloidal matter, and high-molecular-weight organic contaminants.
Feedwater requirements
| Parameter | Requirement |
|---|---|
| Total exchangeable anions, as CaCO₃ | ≤36 ppm |
| Conductivity equivalent | ≤62 μS/cm |
| Temperature | 4.4-40°C / 40-104°F |
| Total hardness, as CaCO₃ | ≤1.0 ppm* |
| Silica, SiO₂ | ≤1.0 ppm** |
| Total organic carbon, as C | ≤0.5 ppm |
| Total chlorine | ≤0.05 ppm |
| Iron, manganese, and hydrogen sulfide | ≤0.01 ppm |
| Boron | ≤1.0 ppm*** |
| pH | 4-11 |
| Oil and grease | None detectable |
| Particulates | RO permeate |
| Oxidizing agents | None detectable |
| Color | ≤5 APHA |
* The 1.0 ppm hardness limit applies to standard counter-current operation. The allowable hardness limit decreases to 0.1 ppm as CaCO₃ in co-current operation.
** The allowable silica limit may decrease at flow rates above 5 m³/h. It may also decrease to 0.5 ppm when feedwater hardness exceeds 0.5 ppm as CaCO₃.
** * When a silica guarantee or a resistivity guarantee above 10 MΩ·cm is required, the boron feed level is limited to 0.3 ppm as B.
RO permeate is specified because the EDI stack contains packed ion exchange media that cannot be backwashed or fluidized to remove particulate contamination. Where an open system exists between the RO unit and the EDI system, such as a storage tank or decarbonator, filtration should be installed immediately upstream of the stack. A 5 μm absolute or 1 μm nominal filter is generally suitable.
Feedwater suitability should be confirmed for the specific application using the Winflows® Design Simulator and the E-Cell™ EDI Stack Owner’s Manual.
Designed for Global Industrial Projects
The E-Cell™ EDI MK-9 Stack is manufactured in facilities certified to ISO 9001 and ISO 14001 standards.
Quality and compliance
CSA and CE compliant
Manufactured in an ISO 9001 and ISO 14001 certified facility
Halal certified by the Islamic Food and Nutrition Council of America, IFANCA®
The MK-9 Stack is also supported by a standard 3-year prorated warranty for leak-free operation.
Make High-Purity Water Easier to Operate
From high-pressure boiler systems to electrolyzer feedwater, the E-Cell™ EDI MK-9 Stack provides the water quality, recovery, and operational simplicity required by modern industrial facilities.
With continuous electrical regeneration, high sodium and silica removal, and no routine acid or caustic regeneration, the MK-9 helps reduce chemical handling while supporting reliable ultrapure water production.
Request an EDI Application Review
Connect with an EDI specialist to evaluate:
Required flow rate and product water quality
Feedwater compatibility
RO and pretreatment requirements
Recovery and operating conditions
System configuration and installation requirements
Available performance guarantees
Send Your Water Treatment Requirement
Tell us the feedwater, required capacity, target water quality and project conditions. Your inquiry email will automatically include the page you are viewing so our team can understand the exact product, technology or reference that led to your request.
- Feedwater source / available analysis
- Design flow or required production capacity
- Target product-water quality or process duty
- Project country, operating conditions and delivery target